


Factory Inspection for Custom Ribbon Orders: Mid-Production Checklist
Evidence and specification note: Color targets, tolerances, test methods, documentation, acceptance criteria, and remedies must be confirmed for the quoted material and written into the approved sample, specification, and sales agreement. General scenarios in this article are not guaranteed production results. Pricing and example note: Current pricing is quoted to specification. Material, width, color, decoration,…
A ribbon factory inspection usually means a third-party agent showing up at the warehouse the day before a container ships. That is too late. By then, the entire 10,000-yard batch is woven, printed, and spooled. Any cost, discount, or savings must be calculated from the dated quotation and the buyer’s approved specification. The fix is not a better pre-shipment checklist. The fix is moving the checkpoint earlier.
Why Mid-Production Inspection Prevents Costly Defects
A mid-production inspection catches defects before the entire batch is committed.
A custom ribbon order is not a single event. It is a manufacturing process with multiple failure points that compound over time. Dye lot drift, weave tension variation, and print registration errors do not happen at once. They creep in. A pre-shipment-only inspection catches defects after the entire batch is already packed, spooled, and ready to ship. At that point, the only options are accept a bad batch or reject it and start over. Both cost money.
- Dye Lot Drift: The approved physical sample is the reference. During production, dye baths can shift. A mid-production check under D65 lighting with a spectrophotometer catches color drift beyond the buyer-approved tolerance before the next 7,000 yards are woven. Fix: stop the line, re-dose the bath, and re-run only the affected rolls.
- Print Registration Errors: Foil stamping and screen printing require precise alignment. A shift of 0.5mm is visible on a luxury box. A mid-production inspection catches misregistration while the print head is still set up. Correction takes hours, not weeks.
- 3M Tape Peel Test: A single tape peel on foil stamping during mid-production can predict adhesion failure before final spooling. If the foil lifts, the line stops and the adhesive or pressure setting is adjusted. This test catches failures that a visual check misses.
- Foreign Object Contamination: Broken weaving pins and human hairs embed in ribbon rolls. Most checklists ignore this. Demand a dedicated visual and metal-detect step during mid-production. A metal shard in a luxury ribbon roll is a brand crisis.
| Inspection Stage | What is Checked | Why it Prevents Defects | Cost of Skipping | Industry Standard |
|---|---|---|---|---|
| Mid-production check | Color match (buyer-approved color tolerance), foil adhesion (3M tape test), print registration, roll edge uniformity | Catches defects before the entire batch is committed; allows real-time rework while the line is running | Any cost, discount, or savings must be calculated from the dated quotation and the buyer’s approved specification. | Confirm buyer requirements in the approved specification |
| Pre-Shipment (Final QC) | AQL sampling to the buyer-approved plan, visual inspection for foreign objects, final color verification | Ensures only conforming product leaves the factory; provides final documented batch record for buyer approval | Quoted after RFQ | Third-party agencies (SGS, BV, Intertek) often only perform this stage; combine with in-house mid-production check for maximum coverage |
| Post-Weaving (Weave Tension Check) | Weave tension variation, yarn breakage, width tolerance | Catches structural defects before printing; prevents print registration errors caused by uneven weave | Print registration errors on finished ribbon: rework or scrap of printed rolls | Confirm buyer requirements in the approved specification |
| Post-Print (Print Quality Check) | Print registration accuracy, ink adhesion, color consistency across the roll, foil stamp clarity | Ensures print quality before final spooling; allows correction of misregistration or fading before bulk production continues | Foil stamp fading or misregistration on entire batch: reprint or scrap cost | Critical for luxury cosmetics and award ribbons |
| Foreign Object Detection | Visual inspection for broken pins, human hairs, metal fragments; metal-detect step | Prevents contamination of ribbon rolls; most checklists ignore this step | Contamination in luxury packaging: brand embarrassment, customer complaints | Demand this step from your supplier; not standard in most factories |
Real Cost of Skipping QC: Batch Rejection Data
many post-production disputes stem from skipped physical samples.
When a buyer approves a digital mockup instead of a woven physical sample, the factory has no calibrated reference for color, hand feel, or print registration. The result: a 10,000-yard satin ribbon batch that drifts buyer-approved ΔE tolerance off target. That batch gets rejected. Any cost, discount, or savings must be calculated from the dated quotation and the buyer’s approved specification.
- Material loss: Current pricing is quoted after the material, width, decoration, quantity, packing, delivery terms, and destination are confirmed.
- Hidden costs: Current pricing is quoted after the material, width, decoration, quantity, packing, delivery terms, and destination are confirmed.
- Inspector cost vs. loss: Quoted after RFQ. Any cost, discount, or savings must be calculated from the dated quotation and the buyer’s approved specification.
Foreign object contamination is another failure mode that pre-shipment inspection routinely misses. Broken loom pins, human hairs, and dust particles get wound into ribbon rolls during weaving. These contaminants only surface when the end-user unspools the ribbon on a high-speed packaging line, causing jams and product damage. Demand a dedicated visual and metal-detect step during mid-production QC. A metal detector pass costs pennies per roll and prevents a claim that could run into five figures.
| Defect Type | Root Cause | Cost of Rejection (10,000 yds) | Detection Point |
|---|---|---|---|
| Color Drift (buyer-approved ΔE tolerance) | Skipped physical sample approval; dye lot variation | Quoted after RFQ | Mid-production check |
| Foil Stamp Fading/Flaking | Incorrect foil/ribbon temperature/pressure | Quoted after RFQ | 3M tape peel test at mid-run |
| Print Registration Error (>0.5mm) | Screen misalignment; material stretch | Quoted after RFQ | Post-print inspection |
| Foreign Object Contamination | Broken pins; human hair from weaving | Quoted after RFQ | Visual + metal-detect step |
| Width Tolerance Drift (>1mm) | Weave tension variation; loom error | Quoted after RFQ | Post-weaving measurement |
In-House vs Third-Party Inspection: Which Is Better?
In-house inspection catches defects mid-run; third-party catches them at the dock.
- Documentation: Demand a signed mid-production inspection report with photos of the approved physical sample, the production roll, and the spectrophotometer reading. The third-party report should include the AQL sampling plan, defect counts by severity, and a pass/fail determination. No report, no shipment.
- The Foil Adhesion Trap: A third-party inspector may perform a tape peel test on one roll. An in-house check can repeat the same test at intervals during the mid-run. If the foil flakes at mid-run, the print head can be adjusted. If it flakes at pre-shipment, the entire batch is scrap.
How to Execute a Mid-Production Ribbon QC Check
- Color match: Place a 12-inch sample from the run next to the approved physical sample under D65 lighting. Measure with a spectrophotometer. Demand buyer-approved ΔE tolerance. If the reading exceeds that tolerance, reject the run and require a dye or ink adjustment before the line resumes.
- Foil adhesion: Apply a strip of 3M 600 tape to the foil-stamped area, press firmly, then peel at a 90-degree angle. If any foil transfers to the tape, the adhesion is failing. Stop the line. This test during mid-production predicts whether the foil will survive spooling, packing, and end-use handling.
- Print registration: Check that all printed elements fall within 0.5 mm of the intended position. Treat misregistration beyond that threshold as a major defect. Measure at both edges and the center of the ribbon width.
- Roll edge uniformity: Inspect the first and last 5 yards of the run for frayed edges, loose weaves, or uneven selvedge. Edge defects compound during re-spooling and cause downstream rejection at the packer or retailer.
Interpreting AQL Standards for Custom Ribbon Orders
Here is the part most procurement managers miss: demand the factory provide the AQL sampling plan in writing before production starts. Not at pre-shipment. Before the first roll is cut. The plan must state the lot size, sample size (per ISO 2859-1), and the accept/reject numbers for each defect class. If the factory cannot produce this document on demand, they do not have a repeatable QC process.
Conclusion
A mid-production inspection catches color drift, foil adhesion failure, and width variance before the entire order is committed. The cost of skipping this step is measured in lost seasons, not just lost material.
Review the Custom Printed Ribbon product page before requesting a sample or quote.
Frequently Asked Questions
How to do on-site pre-shipment inspection for ribbons?
On-site pre-shipment inspection for ribbons involves checking color against the approved sample using a spectrophotometer, verifying width and weave consistency, and testing foil adhesion with a tape pull test. Confirm the inspector has a spectrophotometer and AQL sampling plan before arrival.
Can I send a third-party inspector before shipment?
Yes, you can send a third-party inspector before shipment. However, third-party inspectors typically catch defects only at the dock. Schedule the inspection at least 5 business days before the planned ship date.
What color tolerance is acceptable for custom ribbon?
The acceptable color tolerance for custom ribbon is buyer-approved ΔE tolerance when measured against the approved Pantone standard using a spectrophotometer. Always approve a physical sample before bulk production to lock in the color target.
How are foil adhesion and print quality inspected?
Foil adhesion is inspected using a standard tape pull test to ensure the foil does not peel or fade, and print quality is checked for registration accuracy and clarity against the approved sample. Request a tape pull test report from the factory before shipment.
Keep exploring
Recommended buyer guides
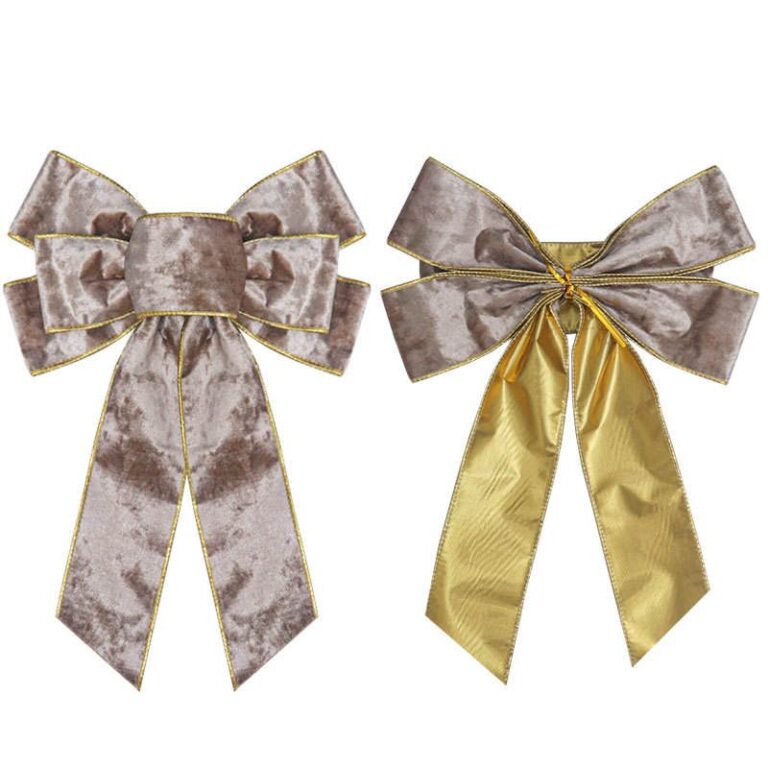 Pre-Tied Bows for Retail Packaging: When They Reduce Labor and Rework
See when pre-tied bows reduce retail packaging labor, improve consistency, and simplify bulk packing, SKU planning, and reorders
Explore guide
 Velvet Ribbon Wholesale Checklist: MOQ, Finish, and Supplier Questions
Evaluate velvet ribbon wholesale options: MOQ, setup fees, unit cost, and packing. Narrow the list before requesting samples…
Explore guide
 Wholesale Custom Ribbon with Logo: Specs, Roll Length, and RFQ Checks
Step-by-step: Custom Ribbon With Logo. Check artwork files, print method, color target, and sample approval to avoid delays,…
Explore guide
 Wholesale Ribbon By The Roll: Roll length and inventory planning
Evaluate Wholesale Ribbon By The Roll options: factory capability, QC proof, lead time, and reorder reliability. Narrow the…
Explore guide
Leave a comment
Share a sourcing question or feedback on this guide. The Lude team reviews submissions before following up.